- English
- French
- German
- Portuguese
- Spanish
- Russian
- Japanese
- Korean
- Arabic
- Greek
- German
- Turkish
- Italian
- Danish
- Romanian
- Indonesian
- Czech
- Afrikaans
- Swedish
- Polish
- Basque
- Catalan
- Esperanto
- Hindi
- Lao
- Albanian
- Amharic
- Armenian
- Azerbaijani
- Belarusian
- Bengali
- Bosnian
- Bulgarian
- Cebuano
- Chichewa
- Corsican
- Croatian
- Dutch
- Estonian
- Filipino
- Finnish
- Frisian
- Galician
- Georgian
- Gujarati
- Haitian
- Hausa
- Hawaiian
- Hebrew
- Hmong
- Hungarian
- Icelandic
- Igbo
- Javanese
- Kannada
- Kazakh
- Khmer
- Kurdish
- Kyrgyz
- Latin
- Latvian
- Lithuanian
- Luxembou..
- Macedonian
- Malagasy
- Malay
- Malayalam
- Maltese
- Maori
- Marathi
- Mongolian
- Burmese
- Nepali
- Norwegian
- Pashto
- Persian
- Punjabi
- Serbian
- Sesotho
- Sinhala
- Slovak
- Slovenian
- Somali
- Samoan
- Scots Gaelic
- Shona
- Sindhi
- Sundanese
- Swahili
- Tajik
- Tamil
- Telugu
- Thai
- Ukrainian
- Urdu
- Uzbek
- Vietnamese
- Welsh
- Xhosa
- Yiddish
- Yoruba
- Zulu
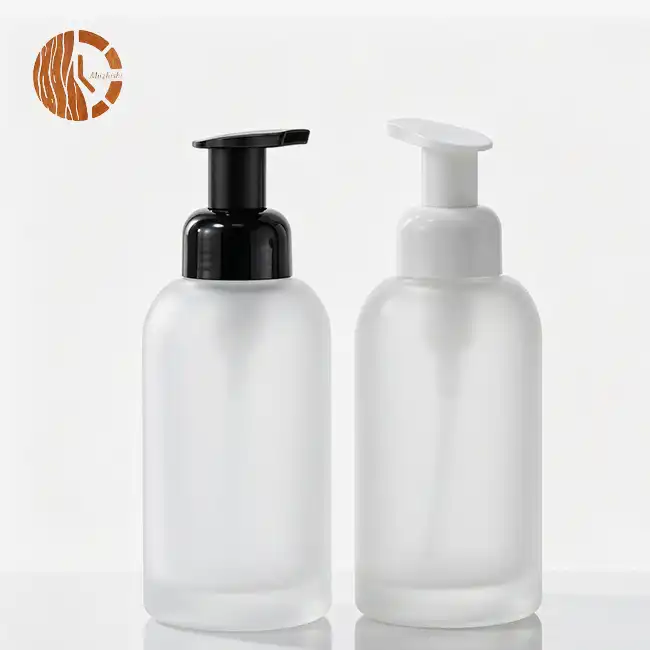
Black Matte Glass Pump Bottle
Color: Transparent,Customized
Usage: Liquid Soap,Lotion ,Hand Wash ,Skin Toner
Customization capability: Hot Stamping, Inside Engraving, Clear, SCREEN PRINTING, Sizes, Colors, Bottle Types, Logo, Sticker or Label, Packing Box, etc
Packaging: As per customer requirements
Transportation method: As per customer requirements Sample:Provided Freely
Black Matte Glass Pump Bottle for Premium Cosmetic Packaging – UV Protection & Customizable Design Solutions
Xuzhou Muzhishi Crafts Co., Ltd. delivers high-performance Black Matte Glass Pump Bottle solutions backed by over 20 years of manufacturing expertise. Our 250ml capacity bottles feature superior UV-blocking properties, filtering wavelengths between 200nm and 400nm to protect photosensitive formulations. We offer competitive prices that are 10% to 15% below the market average. Each furnace can make up to one million units per day, and samples can be sent back in three to five days. Each bottle goes through strict ASTM D3359 adhesive tests and pressure leaking tests at -0.05MPa. This makes sure that global beauty names meet pharmaceutical-grade quality standards.
Why Choose Glass Pump Bottles with Matte Black Finish
In the beauty and personal care industries, the need for high-tech containment solutions keeps growing. Chemical inertness in glass stops phthalates and BPA from moving around, while formula contamination is a risk with plastic options. The matte coating has a Shore D hardness rating, which means it won't scratch easily while being shipped or displayed in stores.
Your customers want both functionality and style. Our bottles have finishes that don't reflect light and keep their high-end shelf appeal. They have a hydrolytic resistance Class HGB1 grade. The pouring pumps can do more than 3,000 actions and can accurately measure out doses from 0.12ml to 2.0ml, which is great for serums and lotions with a thick consistency.
Thermal stability lets hot-filling processes happen without changing the shape of the structure. This technical advantage cuts down on production downtime and makes sure that all of your batches are of the same high quality.
Black Matte Glass Pump Bottle Specifications
| Specification | Details |
|---|---|
| Material | High-quality Glass |
| Capacity | 250ml |
| Height | 11.8cm |
| Diameter | 6.5cm |
| Weight | 200g |
| Model Number | CP-L-007 |
| Brand Name | Muzhishi |
| Color Options | Matte Black, Transparent, Customized |
| Surface Handling | Gold Stamp, Hot Stamping, Silk Screen Printing, Decoration Firing, Heat Transfer Printing, Spraying, Inside Engraving, Clear |
| Place of Origin | Jiangsu, China |
| Customization | Hot Stamping, Inside Engraving, Screen Printing, Sizes, Colors, Logo, Sticker or Label, Packing Box |
Versatile Applications Across Industries
Your product deserves packaging that matches its quality. The Black Matte Glass Pump Bottle excels in multiple professional settings where standard containers fail.
Cosmeceutical Environments: Clinical-grade serums containing retinol or vitamin C require total light occlusion. Our bottles prevent oxidation through complete UV barrier technology, maintaining ingredient potency throughout shelf life.
Luxury Hospitality Settings: High-end hotels and spas demand both aesthetics and durability. The matte texture provides non-slip grip in humid bathroom environments, while glass material resists corrosive effects from organic soaps with elevated salinity levels.
Artisanal Beauty Products: Boutique brands using essential oil blends benefit from glass construction that eliminates environmental stress cracking common in plastic containers. The black matte finish strategically conceals minor sedimentation, preserving premium brand perception.
Advanced Customization Capabilities
We know that the way your brand is known calls for unique package options. With our ODM and OEM services, we can turn your ideas into goods that are ready to sell in just 25 days for unique models.
You can add logos using hot pressing or inside etching methods that leave marks that last. Screen printing can handle complicated graphics, and our 3D printing support lets you make quick prototypes of structures with unusual designs.
You can change the colour to any Pantone reference, not just standard black matte. The bottle sizes can be changed to fit your needs, from small 30ml sample sizes to large 500ml shop sizes.
Your dedicated account manager handles all the details, from the first sketches of an idea to the final packaging requirements. This personalised method gets rid of the contact problems that come up with buying from more than one seller.

Uncompromising Quality Assurance
Systematic tests that go beyond international standards are done on every Glass Pump Bottle. Cross-cut tape testing according to ASTM D3359 makes sure that the coating will stick in chemically-rich situations that your formulas may face.
Testing for vacuum leakage at -0.05MPa for five minutes makes sure that the seal stays intact while air is being transported. This keeps expensive goods from going missing and keeps customers from being unhappy with damaged shipments.
Dosage precision within a ±5% range is guarantyd by pump priming analysis. Ultrasonic sensors check the spread of wall thickness to keep things from breaking on your production facility's high-speed automatic closing lines.
Accelerated ageing tests that last for 12 weeks show that recipes will not react with NBR or Viton internal gaskets. This proactive method keeps your brand's image safe and cuts down on warranty claims.

Sustainable and Recyclable Design
Environmental responsibility doesn't compromise luxury aesthetics. Our organic frosted coatings burn off cleanly during glass cullet melting processes, maintaining 100% recyclability status.
Glass provides indefinite reuse potential without quality degradation. Your environmentally conscious customers appreciate packaging that aligns with zero-waste values while delivering premium functionality.
The durable construction encourages consumers to repurpose bottles after initial product consumption. This extended lifecycle reinforces positive brand associations and reduces landfill contributions.

Streamlined Global Logistics
International shipping problems shouldn't hold up the start of your products. Our full export help includes clearing customs, coordinating inspections, and setting up multimodal transport.
We offer complete documentation packages that include commercial invoices, packing lists, and certificates of origin that are made to fit the needs of the country where the goods are going. This attention to regulatory details speeds up the customs process and keeps shipments from being held up.
Items that are in stock ship right away, and special orders have clear lead times: samples in about 25 days, and mass production within 30 days after approval. Our six automated lines per furnace make sure that both new orders and reorders are delivered on time every time.
Frequently Asked Questions
Q: Does the matte coating affect recycling capabilities?
A: Modern organic frosted coatings completely burn off during glass melting processes, maintaining full recyclability without contaminating cullet streams.
Q: How do you prevent pump clogging with thick formulations?
A: We engineer back-flow prevention valves with orifice diameters specifically calculated for your product's centipoise rating, ensuring smooth dispensing regardless of viscosity.
Q: Will the finish withstand alcohol-based sanitizers?
A: Our chemical-resistant coatings pass 24-hour alcohol immersion testing without softening or discoloration, ideal for sanitization-focused product lines.
Q: Are internal components BPA-free?
A: All dip tubes and pump mechanisms use FDA-compliant food-grade PE/PP materials, guaranteeing zero endocrine disruptor leaching into your formulations.
Q: What protects bottles during shipping?
A: We apply secondary UV-cured topcoats passing 3H pencil hardness tests, combined with custom packaging solutions that prevent transit damage.
Partner with Proven Manufacturing Excellence
Transform your packaging strategy with solutions designed for demanding global markets. Our integrated approach combines technical precision, aesthetic sophistication, and reliable supply chain management.
Contact us today at long@muzhishi.com to request free samples and discuss how our Black Matte Glass Pump Bottle solutions can elevate your brand positioning.

Our customers’ satisfaction speaks for our quality — contact us to experience the same reliable service.